In resin-bonded foundries, sand mixing is not simply about putting sand and resin together.
The real challenge is uniform binder distribution, stable mixing time, accurate dosing, repeatable sand quality, and sufficient production capacity.
If the mixing process is unstable, the problems usually appear later:
Poor mold or core strength
Uneven curing
Excessive resin consumption
Short or inconsistent bench life
Sand sticking
Unstable casting quality
More rejected molds and castings
Higher production cost
Double Sleeve Resin Sand Mixing Machine is designed for foundries that need more controlled resin sand preparation, especially for phenolic resin, furan resin, no-bake sand, and other resin-bonded sand processes.
The key is not simply choosing a larger mixer.
The key is matching the mixer structure + sand condition + resin system + production rate + mixing time + discharge method to the actual foundry process.
What Is a Double Sleeve Resin Sand Mixing Machine?
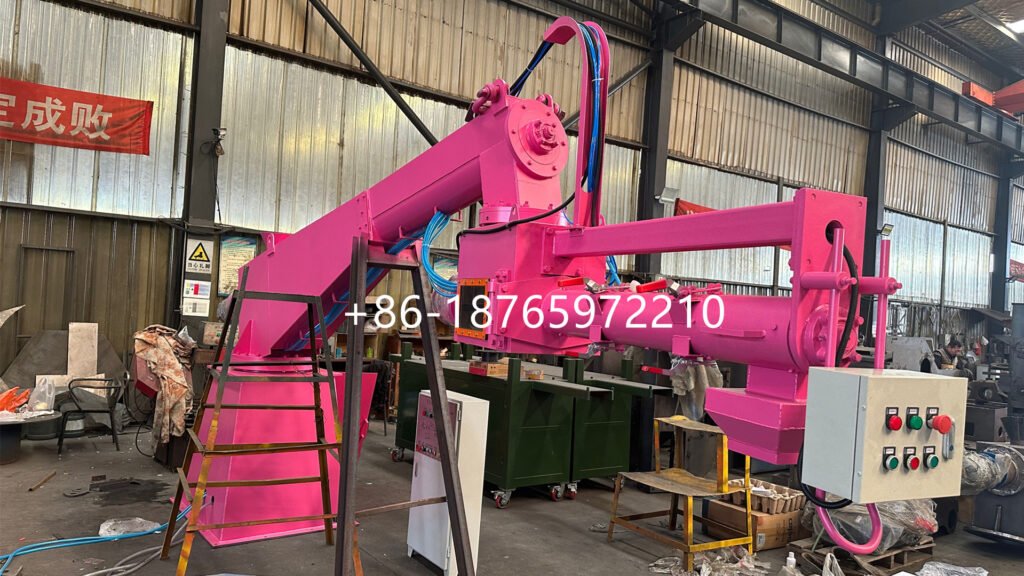
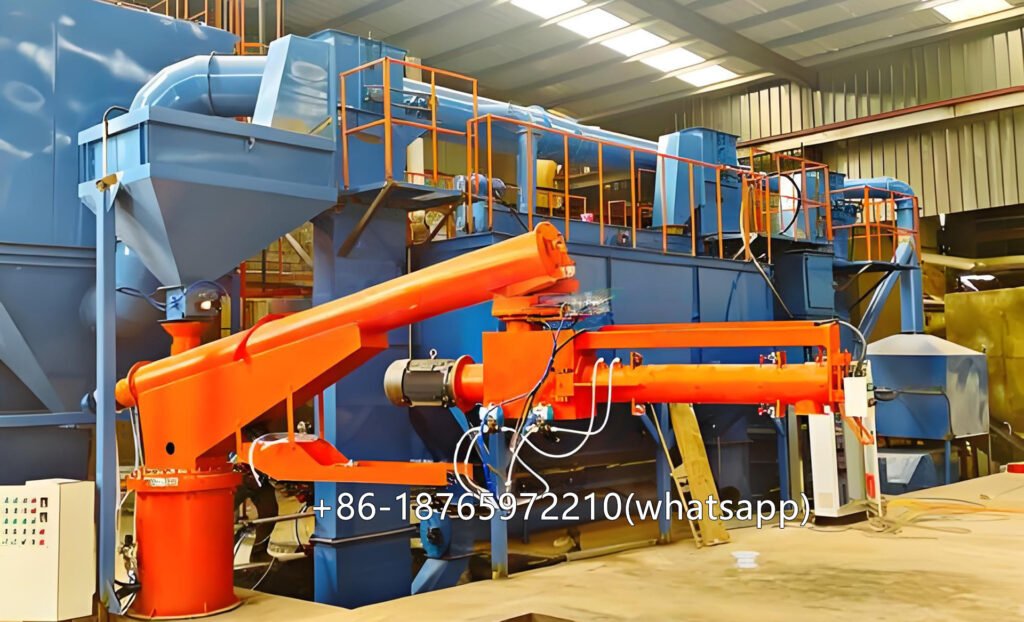
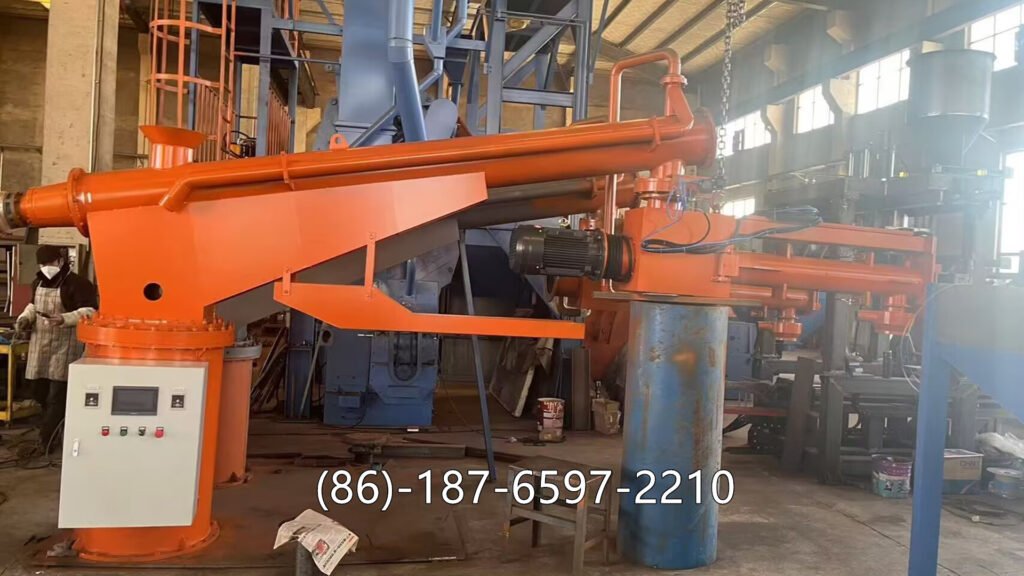
Double sleeve resin sand mixing machine is a mechanical foundry sand mixer designed to mix sand with liquid binders such as resin and catalyst/hardener.
The machine typically consists of:
Mixing chamber
Double-sleeve or double-arm mixing structure
Mixing blades/shafts
Sand inlet
Resin dosing system
Catalyst/hardener dosing system
Discharge mechanism
Drive motor
Control cabinet
Safety protection system
The machine mixes sand and binder mechanically until the required coating and distribution are achieved.
ISO 23062:2022 specifically covers foundry machinery used for conditioning and reclaiming foundry sands and defines a sand mixer as equipment in which sand and bonding agents are mixed and conveyed to the discharge gate, including batch and continuous types.
For buyer, this distinction is important:
The mixer should be selected according to the actual sand preparation process, not only according to the nameplate capacity.
Why Phenolic Resin Sand Preparation Needs Better Mixing Control
Phenolic resin systems are sensitive to process conditions.
The final sand performance can be affected by:
Sand temperature
Sand moisture
Reclaimed sand percentage
Resin dosage
Catalyst/hardener dosage
Mixing sequence
Mixing time
Discharge time
Ambient temperature
Sand particle characteristics
A mixer that does not distribute binder evenly may create two problems at the same time:
Too little binder in one area → insufficient strength
Too much binder in another area → unnecessary material consumption and curing problems
Therefore, the objective of a resin sand mixer is not simply:
How Does a Double Sleeve Resin Sand Mixing Machine Work?
A typical working sequence is:
Step 1 — Sand Loading
New sand, reclaimed sand, or a controlled blend is loaded into the mixing chamber.
For many foundries, reclaimed sand is mixed with new sand to reduce material consumption.
Step 2 — Dry Sand Mixing
The mixer starts mechanical agitation to distribute the sand evenly before binder addition.
This step is particularly useful when the incoming sand contains differences in temperature, moisture, or reclaimed-sand proportion.
Step 3 — Resin Addition
The resin system is introduced according to the process recipe.
The actual dosage should be determined according to the binder manufacturer’s technical data and the required mold/core performance.
Step 4 — Catalyst or Hardener Addition
Catalyst or hardener is added according to the selected resin system.
For no-bake processes, the relationship between resin, catalyst and working time is especially important.
Step 5 — Intensive Mixing
The double-sleeve mixing structure continuously moves the sand through the mixing zone.
The purpose is to improve contact between:
Sand grains → Resin → Catalyst/Hardener
Step 6 — Discharge
The finished resin sand is discharged directly to:
Molding equipment
Coremaking equipment
Sand conveyor
Sand hopper
Manual molding station
Automatic molding line
The shorter and more controlled the transfer path, the easier it is to maintain process consistency.
Why Choose a Double Sleeve Resin Sand Mixer?
The double-sleeve configuration can be considered when the foundry requires more effective mixing and higher process stability than a simple single-sleeve configuration can provide.
1. More Uniform Binder Distribution
The mixing structure repeatedly moves sand through the active mixing zone.
This helps distribute resin and catalyst across the sand mass.
Uniform distribution is particularly important for resin-bonded molds and cores where local binder concentration can affect strength and curing.
2. Better Mixing Efficiency
A well-designed double-sleeve mixer can provide intensive movement of the sand while maintaining a controlled mixing cycle.
The objective is to achieve the required sand quality within the available production cycle.
However, shorter mixing time is not automatically better.
The correct mixing time must be established through actual process testing.
3. Suitable for Reclaimed Sand
Many foundries use reclaimed sand to reduce the consumption of new sand.
The mixer must therefore handle the actual reclaimed-sand characteristics rather than only fresh sand.
Important variables include:
Reclaimed sand temperature
Residual binder
Grain size distribution
Moisture
Fines content
New/reclaimed sand ratio
4. Better Control of Resin Consumption
Binder cost can become a significant part of resin sand production cost.
The objective should not be to simply add more resin.
Instead:
Use the minimum practical binder dosage required to achieve the specified process performance.
Accurate dosing and uniform distribution can help reduce over-dosing caused by inconsistent mixing.
Typical Technical Parameters
The following values are typical engineering reference ranges, not universal specifications. Final parameters should be selected according to sand type, binder system, required throughput, batch size and customer process.
Parameter
Typical Reference
Machine Type
Double Sleeve Resin Sand Mixing Machine
Application
Resin-bonded foundry sand
Main Materials
New sand / reclaimed sand / blended sand
Binder
Phenolic / furan / other resin systems
Catalyst
Process-dependent catalyst or hardener
Batch Capacity
Approx. 100–1000 kg/batch
Production Capacity
Approx. 2–15 tons/hour
Main Motor
Approx. 11–45 kW
Mixing Time
Process-dependent
Dosing System
Manual / automatic
Discharge
Pneumatic / hydraulic / mechanical
Control
Electrical / PLC + HMI optional
Sand Temperature
Process-dependent
Sand Ratio
New + reclaimed sand, according to process
Installation
Stand-alone / integrated production line
Customization
Available according to process requirements
Important:
Do not select the mixer only by tons/hour.
A 10 t/h mixer does not necessarily produce 10 tons of qualified resin sand per hour under every operating condition.
Actual output depends on:
Batch loading
Mixing time
Loading time
Binder dosing time
Discharge time
Operator handling
Molding demand
Reclaimed sand condition
Required sand quality
How to Calculate Resin Sand Mixer Capacity
For batch mixing equipment, a useful engineering calculation is:
Actual Production Capacity ≈ Effective Batch Weight × 60 / Total Cycle Time
Where:
Total Cycle Time = Loading + Dry Mixing + Binder Dosing + Wet Mixing + Discharge
For example:
Effective batch weight: 500 kg
Total cycle time: 6 minutes
The theoretical output is:
500 × 60 / 6 = 5,000 kg/h
or approximately:
5 tons/hour
But this is a theoretical calculation.
Actual production should include loading interruptions, material variation, operator handling and other production losses.
Therefore, when purchasing a mixer, ask the manufacturer for:
Rated capacity + recommended batch weight + cycle time + actual test results.
Mixing Time Is More Important Than Motor Power
One common purchasing mistake is comparing resin sand mixers only by motor power.
A 30 kW motor does not automatically mean better mixing than a 22 kW motor.
The mixer therefore becomes one part of a larger sand-management system.
For a complete production line, the mixer may need to connect with:
Sand reclamation system
Sand cooler
Magnetic separator
Sand storage hopper
Weighing system
Resin pump
Catalyst pump
Pneumatic conveying
Molding station
This is why a B2B quotation should evaluate the complete material flow, not just the mixer itself.
Double Sleeve vs Single Sleeve Resin Sand Mixer
Which one should a foundry choose?
The answer depends on the production process.
Factor
Single Sleeve
Double Sleeve
Machine Structure
Simpler
More intensive mixing configuration
Investment
Usually lower
Usually higher
Mixing Requirement
Standard
Higher mixing demand
Production Scale
Small/medium
Medium/high depending model
Binder Distribution
Process-dependent
Designed for intensive mixing
Reclaimed Sand
Suitable with proper control
Suitable with proper control
Automation
Optional
Optional
Customization
Available
Available
The correct choice should be based on:
Required output + batch size + binder system + sand condition + mixing cycle + available space + budget.
How to Reduce Foundry Sand Mixing Costs
A high-conversion equipment purchase is not about buying the cheapest mixer.
It is about reducing the total cost per ton of qualified resin sand.
Consider these cost factors:
1. Resin Consumption
Poor mixing may encourage operators to increase resin dosage.
Better process control can help avoid unnecessary over-dosing.
2. Electricity
Motor power and operating time both affect energy consumption.
3. Sand Loss
Effective reclamation and controlled sand preparation can reduce new sand consumption.
4. Rejected Molds
Inconsistent sand quality can result in:
Poor mold strength
Cracks
Sand erosion
Casting defects
Rework
5. Maintenance
The cost of wear parts, seals, bearings, mixing tools and liners should be considered.
6. Labor
Automatic dosing and automatic discharge can reduce repetitive manual operations.
Key Wear Parts of a Resin Sand Mixer
Before purchasing, ask the supplier which parts are considered wear parts.
Typical items may include:
Mixing blades
Mixing tools
Liners
Shafts
Bearings
Seals
Discharge components
Pump components
Flexible hoses
The material and thickness of wear components should be selected according to:
Sand abrasiveness
Reclaimed sand content
Operating hours
Batch size
Binder characteristics
A machine with a low initial price but expensive or difficult-to-source wear parts may have a higher long-term operating cost.
Maintenance Checklist
A practical maintenance program should include:
Daily
Check abnormal noise
Check vibration
Inspect discharge gate
Check resin/catalyst leakage
Clean residual sand
Inspect safety devices
Weekly
Inspect mixing tools
Check bearings
Inspect seals
Check dosing pipes
Check pump operation
Monthly
Check motor and gearbox
Inspect shaft condition
Check electrical connections
Verify dosing accuracy
Inspect wear liner thickness
Periodically
Calibrate dosing system
Replace worn mixing tools
Check gearbox oil
Check safety interlocks
Inspect complete mixer structure
Maintenance intervals should be adjusted according to actual operating hours and manufacturer recommendations.
Safety Requirements for Resin Sand Mixing Equipment
Safety should be considered during equipment design, installation, operation and maintenance.
ISO 23062:2022 addresses foreseeable hazards for foundry machinery used for sand conditioning/reclamation, molding and coremaking, and incorporates risk-reduction principles associated with ISO 12100. It also points to IEC 60204-1:2016 for electrical hazards.
A resin sand mixer should typically include appropriate:
Guards
Emergency stop devices
Access-door interlocks where applicable
Inspection openings
Motor overload protection
Electrical protection
Safe maintenance access
Warning labels
Lockout/tagout procedures
For resin systems, the buyer should also consider the SDS and handling requirements of the specific resin and catalyst products.
The equipment manufacturer should not assume that every resin system has identical chemical or ventilation requirements.
CE and European Machinery Compliance
For machines supplied to the European market, buyers should distinguish between CE marking and a generic “CE certificate.”
Regulation (EU) 2023/1230 establishes machinery conformity requirements and requires manufacturers to ensure applicable essential health and safety requirements are fulfilled, prepare technical documentation, complete the relevant conformity assessment procedure, and affix the CE marking where applicable.
For an EU-bound resin sand mixer, ask the supplier for the applicable technical compliance documentation, including:
Risk assessment
Technical documentation
Declaration of Conformity
User manual
Electrical documentation
Safety-related information
CE marking information, where applicable
The exact conformity route depends on the machinery and its applicable regulatory classification.
ISO 9001:2026 and Foundry Equipment Quality Control
ISO 9001:2026 was published on September 16, 2026 and replaces ISO 9001:2015. The new edition continues to provide a framework for establishing, implementing, maintaining and continually improving a quality management system.
For a machinery buyer, ISO 9001 certification should not be treated as a substitute for equipment testing.
Instead, ask the manufacturer how its quality system controls:
Raw material purchasing
Welding
Machining
Assembly
Electrical installation
Supplier components
Inspection
Factory testing
Final documentation
Customer complaints
Corrective actions
The important question is:
Can the supplier show a repeatable manufacturing and inspection process for the actual machine you are buying?
Factory Acceptance Test for a Double Sleeve Resin Sand Mixer
Before shipment, a B2B buyer should request a factory acceptance test whenever practical.
A useful FAT checklist includes:
Mechanical Test
No abnormal vibration
No abnormal noise
Smooth shaft rotation
Stable discharge
Proper opening/closing of discharge mechanism
Electrical Test
Motor current
Rotation direction
Emergency stop
Interlock function
Control panel operation
PLC/HMI functions if included
Mixing Test
Use the customer’s actual or representative:
Sand
Resin
Catalyst
Reclaimed sand ratio
Then evaluate:
Mixing time
Binder distribution
Discharge consistency
Sand temperature
Final mold/core performance
For serious foundry projects, testing with actual process materials is much more valuable than relying only on an empty-machine running test.
How to Choose the Right Double Sleeve Resin Sand Mixer
Before requesting a quotation, prepare these 10 parameters:
Required capacity: ___ tons/hour
Batch size: ___ kg/batch
Sand type: New / reclaimed / blended
Reclaimed sand percentage: ___%
Resin type: Phenolic / Furan / Other
Catalyst type: ___
Binder dosage: ___%
Required mixing time: ___ seconds/minutes
Sand temperature: ___ °C
Discharge height: ___ mm
Also provide:
Available installation space
Existing sand reclamation equipment
Sand cooler information
Existing resin/catalyst pumps
Required automation level
Voltage/frequency
Local safety requirements
Desired delivery time
This information allows the supplier to recommend a machine based on the actual process rather than simply sending a standard catalog model.
Custom Double Sleeve Resin Sand Mixing Machine
For different foundries, the same mixer model may require different configurations.
A supplier should be able to explain what materials are required for a meaningful test.
What is the recommended batch size?
Do not confuse maximum chamber capacity with recommended working capacity.
What mixing time do you recommend?
Ask for the basis of the recommended cycle time.
Can the mixer handle reclaimed sand?
Provide your actual reclaimed-sand percentage and characteristics.
How accurate is the binder dosing?
Ask how dosing accuracy is measured and verified.
What are the main wear parts?
Request material, dimensions and expected service life.
Can the machine connect to our existing sand system?
Provide the existing layout and discharge height.
What documentation is supplied?
For export projects, documentation can be as important as the machine itself.
FAQ: Double Sleeve Resin Sand Mixing Machine
What is a double sleeve resin sand mixing machine?
It is a foundry sand mixer designed to mechanically mix sand with liquid resin and catalyst/hardener for resin-bonded molding and coremaking processes.
Can it mix phenolic resin sand?
Yes, it can be configured for phenolic resin systems when the mixer design and dosing system are compatible with the customer’s specific resin and catalyst.
Can it process reclaimed sand?
Yes. New sand, reclaimed sand or blended sand can be processed, provided the mixer is selected according to the actual sand characteristics and process requirements.
What is the capacity of a double sleeve resin sand mixer?
Typical equipment can range from small batch machines to high-capacity production systems. As an engineering reference, approximately 100–1000 kg/batch and 2–15 tons/hour may cover a range of configurations, but the final capacity must be confirmed through process requirements and testing.
How much resin should be added?
There is no universal resin dosage. The correct dosage depends on the resin system, sand characteristics and required mold/core properties. The resin supplier’s technical data and actual foundry testing should be used.
Can the mixer be automated?
Yes. Options can include automatic sand weighing, resin dosing, catalyst dosing, PLC control, HMI operation and recipe management.
What standards should buyers consider?
ISO 23062:2022 is directly relevant to safety requirements for foundry machinery used for sand conditioning/reclamation, molding and coremaking. Electrical safety requirements should also be considered according to the applicable electrical standard and market requirements.
For EU market placement, Regulation (EU) 2023/1230 establishes machinery safety and conformity requirements, including applicable conformity assessment and CE marking requirements.
We’re here to help! Whether you need more information about our products or services, our team is ready to assist. Don’t hesitate to reach out—we’re just a message away!