
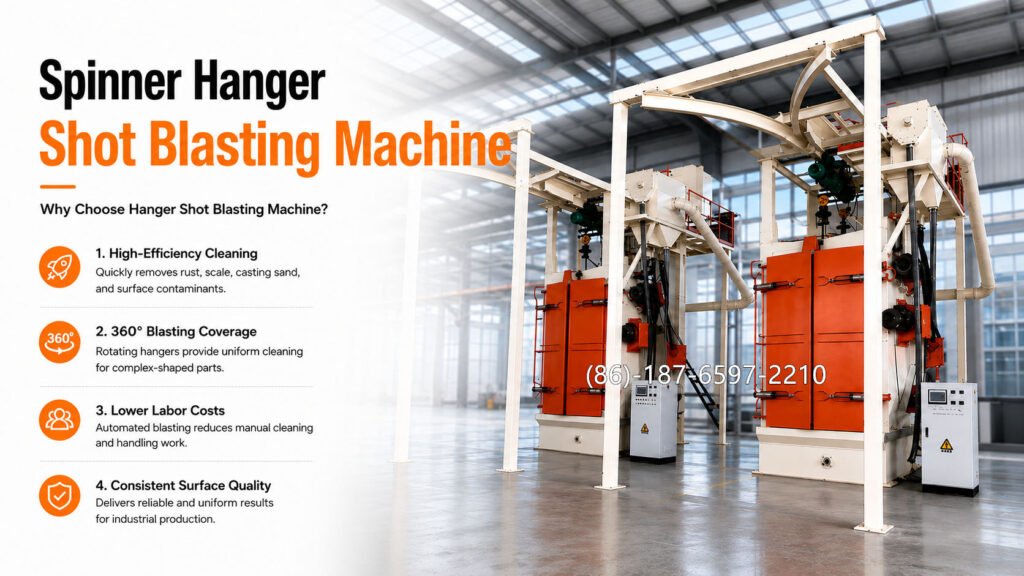
Introduction: Why Is a Hook Type Shot Blasting Machine Important for Surface Preparation?
Rust, mill scale, casting sand, and heat-treatment oxide can reduce the quality of metal parts and affect the adhesion of protective coatings. For foundries, steel fabrication plants, and metalworking factories, manual grinding and cleaning may require significant labor and cannot always deliver consistent results.
A hook type shot blasting machine provides a mechanical solution for cleaning castings, forgings, welded steel structures, and other metal components before painting, coating, inspection, or further processing.
Unlike a tumble shot blasting machine, which cleans parts in a rotating drum, a hook shot blasting machine suspends workpieces from a hook or hanger. During blasting, the hook can rotate to expose different surfaces to the abrasive stream. This arrangement is particularly useful for large, heavy, slender, or easily damaged parts that should not collide with one another.
For manufacturers purchasing surface preparation equipment, the main question is not simply how powerful the blasting wheel is. It is whether the complete machine can achieve the required surface cleanliness, provide adequate coverage, handle the workpiece safely, and maintain the required production output.
This guide explains how a hook type shot blasting machine works, which technical parameters matter, how to select the correct configuration, and which surface preparation standards should be considered before purchasing.
1. What Is a Hook Type Shot Blasting Machine?
Hook type shot blasting machine is an enclosed abrasive blasting system that uses a suspended hook to carry metal workpieces into a blasting chamber.
The machine typically consists of:
- Blast chamber with wear-resistant internal protection
- One or more centrifugal blasting wheels
- Hook, hoist, and conveying mechanism
- Abrasive circulation and recovery system
- Bucket elevator and abrasive separator
- Dust collection system
- Electrical control system and safety interlocks
The Q37 series is a common configuration for this type of equipment. Different models are available for different workpiece diameters, heights, loading capacities, and production requirements.
The machine is commonly used in foundries, machinery manufacturing, automotive component production, steel fabrication, mining equipment manufacturing, and other industries that require repeatable metal surface preparation.
Key purchasing consideration: Select the machine according to the maximum workpiece envelope, loaded weight, shape, cleaning requirement, and batch output—not just the machine model number.
2. How Does a Hook Type Shot Blasting Machine Improve Surface Preparation?
2.1 Removes Rust, Mill Scale, and Surface Contaminants
During operation, the blasting wheels accelerate steel shot or another suitable abrasive and project it toward the workpiece surface at high speed.
Repeated abrasive impact removes loose rust, oxide scale, casting sand, and other contaminants. The actual result depends on the initial surface condition, abrasive type and condition, wheel performance, exposure time, and workpiece geometry.
For steel parts that will be painted or coated, this process provides a controlled preparation method before the next manufacturing stage.
Compared with manual cleaning, an appropriately designed automatic blasting system can reduce dependence on individual operator technique and improve repeatability between batches.
2.2 Improves Coverage on Complex Metal Parts
One major advantage of a hook type shot blasting machine is its suspended workpiece arrangement.
The hook can rotate during blasting, helping expose different sides of a component to the abrasive stream. Multiple blasting wheels may be positioned to cover different areas of the chamber.
This arrangement is suitable for components such as:
- Cast iron and steel castings
- Forged metal parts
- Welded frames and structural components
- Valve bodies and pump housings
- Automotive and machinery components
- Heat-treated metal parts
However, hook rotation alone does not guarantee complete cleaning. Deep recesses, blind holes, overlapping parts, and shielded surfaces may still receive insufficient abrasive impact.
For complex components, the loading arrangement, hook speed, wheel positions, and blasting cycle should be evaluated through a workpiece trial.
2.3 Reduces Workpiece Collision and Handling Damage
Tumble blasting is effective for many small, durable components, but parts collide during the tumbling process.
A hook type shot blasting machine keeps workpieces suspended rather than allowing them to tumble together. This is an advantage when processing:
- Thin-walled castings
- Long or slender components
- Large welded structures
- Precision-machined parts requiring careful handling
- Components with protrusions or relatively fragile features
The suspension method can reduce collision-related damage. Nevertheless, each component must be securely attached, and the hook loading capacity must not be exceeded.
For small parts, a properly designed basket or fixture may also be considered, provided it does not prevent the abrasive from reaching the required surfaces.
2.4 Creates a Suitable Surface for Protective Coatings
Surface cleanliness and surface profile are two different requirements.
Abrasive blasting can remove contaminants and produce a surface texture suitable for many coating systems. However, the required cleanliness grade and profile depend on the coating specification, substrate, abrasive, and service environment.
A surface may look clean but still have an unsuitable profile or contain non-visible contaminants. For critical coating applications, visual inspection should therefore be combined with the appropriate inspection methods.
The target should be defined before production—for example, a specified visual cleanliness grade and an acceptable surface profile range.
2.5 Improves Production Consistency and Reduces Manual Work
Once the blasting cycle, loading arrangement, abrasive flow, and hook rotation have been established, the machine can process repeat batches using a controlled procedure.
This helps manufacturers standardize cleaning operations and reduce repeated manual grinding or brushing.
Actual productivity depends on several factors:
- Number and capacity of blasting wheels
- Workpiece size and loading weight
- Loading and unloading time
- Required cleaning grade
- Abrasive circulation efficiency
- Frequency of abrasive and wear-part maintenance
For factories with a steady flow of different metal parts, a correctly sized hook type shot blasting machine can improve production organization and reduce surface preparation bottlenecks.
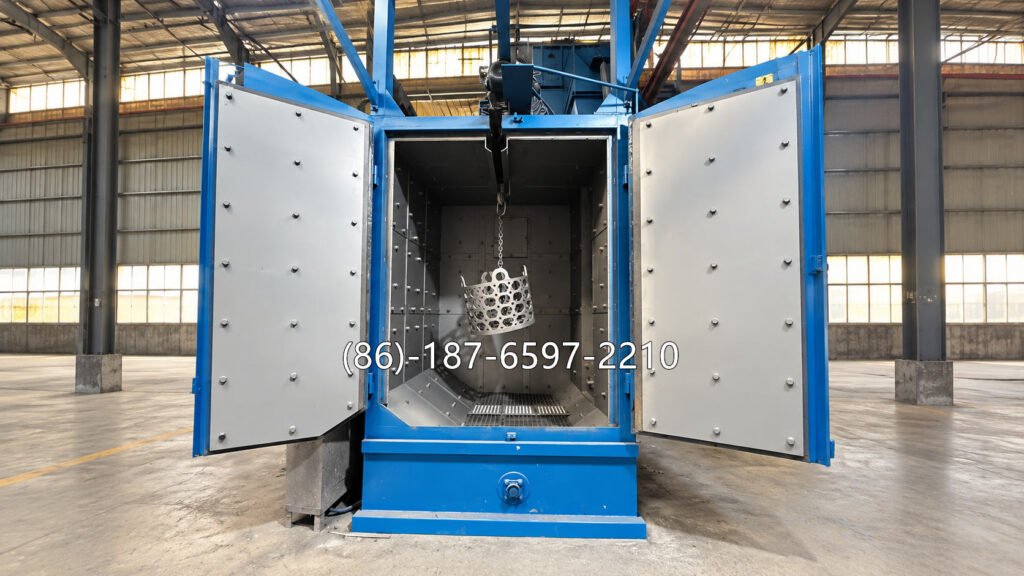
3. How Does a Hook Type Shot Blasting Machine Work?
A typical hook shot blasting cycle follows these steps.
Step 1: Load the workpieces.
The operator or handling system attaches the components to the hook. Parts should be spaced to avoid excessive overlap and allow abrasive access.
Step 2: Move the hook into the chamber.
The hoist or conveying system positions the loaded hook inside the blasting chamber. The access door closes, and the safety interlocks confirm that the machine is ready to operate.
Step 3: Start abrasive blasting.
The blasting wheels accelerate the abrasive and project it onto the exposed workpiece surfaces. Hook rotation helps improve coverage.
Step 4: Recover and separate the abrasive.
Reusable abrasive is collected and returned through the recovery system. The separator removes dust, broken abrasive, and other unwanted material to maintain usable abrasive quality.
Step 5: Extract dust.
The dust collection system removes airborne particles generated during blasting and abrasive separation.
Step 6: Inspect and unload.
After the blasting cycle ends and the system reaches a safe condition, the workpieces are removed and inspected against the specified cleanliness and surface profile requirements.
The complete system—not just the blasting wheel—determines the final cleaning result. Abrasive condition, separation efficiency, dust extraction, sealing, hook rotation, and maintenance all affect operating performance.
4. Typical Technical Parameters of a Hook Type Shot Blasting Machine
The following table provides representative engineering reference ranges for preliminary equipment selection. These are not guaranteed specifications for every Q37 model. The final configuration should be confirmed against the supplier’s technical drawing and quotation.
| Technical parameter | Preliminary reference |
|---|---|
| Machine series | Q37 hook type |
| Workpiece type | Castings, forgings, welded structures, metal components |
| Maximum workpiece envelope | Approximately Ø600–2,000 mm; height about 1,100–3,000 mm across different model configurations |
| Maximum hook load | Approximately 500–10,000 kg across different configurations |
| Number of blasting wheels | Commonly 2–4, depending on model |
| Abrasive flow rate | Approximately 240–1,000 kg/min total across selected configurations |
| Abrasive type | Selected steel shot, steel grit, or other compatible abrasive |
| Hook rotation speed | Model-dependent; commonly a few revolutions per minute |
| Dust collection airflow | Approximately 5,000–28,000 m³/h across selected configurations |
| Control system | Electrical control with appropriate safety interlocks; PLC available where specified |
Reference for model-dependent technical data: Hook Type Shot Blasting Machine technical parameters and Q37 Series Hook Type Shot Blasting Machine.
Important: Workpiece dimensions, hook load, blasting capacity, airflow, and installed power are separate specifications. A machine that can carry a 1,000 kg load does not necessarily have enough blasting capacity to clean every 1,000 kg batch within the desired cycle time.
Before placing an order, ask the manufacturer to confirm the maximum workpiece diameter and height, permitted total load, wheel motor power, abrasive flow, dust collector configuration, and expected cycle time for your actual components.
5. Which Surface Preparation Standards Should Be Considered?
For equipment used before painting or protective coating, the target surface condition should be specified by the project owner, coating manufacturer, or applicable engineering specification.
The following standards are useful starting points.
ISO 8501-1: Visual Assessment of Surface Cleanliness
ISO 8501-1 provides visual assessment criteria for rust grades and preparation grades of steel surfaces, including surfaces prepared by abrasive blast cleaning.
Commonly specified blast-cleaning grades include:
- Sa 1: Light blast cleaning
- Sa 2: Thorough blast cleaning
- Sa 2½: Very thorough blast cleaning
- Sa 3: Blast cleaning to visually clean steel
The required grade must be selected according to the coating specification and project requirements. Do not assume every hook type shot blasting machine automatically achieves Sa 2½ or Sa 3 under all operating conditions.
AMPP / SSPC-SP 10/NACE No. 2: Near-White Metal Blast Cleaning
SSPC-SP 10/NACE No. 2 addresses near-white metal blast cleaning of carbon steel using dry abrasive blasting. It defines the required surface condition and the procedures used to achieve and verify that condition.
It is relevant when the project specification requires near-white metal cleanliness before applying a protective coating.
Official references:
Surface Profile and Additional Inspection
Surface cleanliness does not establish surface profile by itself. If the coating specification requires a particular roughness range, the profile should be measured using an appropriate method and instrument.
Depending on the application, additional checks may include soluble salt testing, dust assessment, and verification of abrasive contamination.
Engineering recommendation: Confirm the cleanliness grade, profile range, inspection method, and acceptance criteria before machine selection. Standards define the required result; machine parameters and process trials determine whether a specific installation can consistently achieve it.
6. Hook Type vs. Tumble Type Shot Blasting Machine
| Comparison item | Hook type | Tumble type |
|---|---|---|
| Workpiece handling | Suspended from a hook or fixture | Parts tumble inside a rotating drum |
| Typical applications | Large, heavy, slender, or collision-sensitive parts | Small, durable, batch-loaded components |
| Workpiece collision | Reduced when parts are properly suspended | Parts contact and collide during tumbling |
| Complex shapes | Good when surfaces are exposed to the abrasive stream | Depends on part geometry and tumbling behavior |
| Loading method | Hoist or hook conveying system | Batch loading into drum or belt |
| Production method | Batch processing; multi-hook arrangements may improve workflow | Batch processing |
| Key selection factor | Workpiece envelope, load, and coverage | Batch weight, part durability, and drum capacity |
Which machine should you choose?
Choose a hook type shot blasting machine if your components are too large, too long, too heavy, or too sensitive to collision for effective tumble blasting.
Choose a tumble type shot blasting machine when you need to process many small, robust parts in batches and the parts can withstand mutual contact.
For mixed production, evaluate the largest component and the most difficult cleaning requirement first. A machine that handles the smallest parts efficiently may not be suitable for your largest workpiece.
7. How to Select the Right Hook Type Shot Blasting Machine
7.1 Confirm the Maximum Workpiece Dimensions
Provide the maximum diameter, length, height, and overall envelope of the workpiece.
The chamber must provide enough clearance for the part, hook, fixtures, and rotation. Long or irregular components may require a customized chamber or suspension arrangement.
7.2 Calculate the Required Hook Load
Determine both the maximum individual component weight and the total suspended load.
Include the weight of the fixture or basket where applicable. If multiple parts are processed together, check the total load and the load distribution.
7.3 Select the Blasting Wheel Configuration
Blasting wheel quantity, motor power, abrasive flow, and installation positions should match the component geometry and required production output.
More blasting wheels do not automatically mean better cleaning. Their positions and abrasive impact directions must provide effective coverage.
7.4 Specify the Surface Preparation Requirement
Tell the manufacturer whether the parts require removal of loose rust, mill scale, casting sand, or previous coatings. For coated steel, identify the required cleanliness grade and surface profile.
Where a strict acceptance criterion applies, arrange a sample test using representative workpieces.
7.5 Match the Dust Collector and Abrasive Recovery System
The separator must remove broken abrasive and contaminants effectively, while the dust collector must suit the machine’s airflow requirements and operating environment.
Insufficient dust extraction or poor abrasive separation can affect visibility, abrasive consumption, and cleaning consistency.
7.6 Confirm the Actual Cycle Time
Ask the supplier to estimate the complete cycle, including loading, chamber movement, blasting, unloading, and any required inspection.
Do not compare machines using blasting time alone. Total cycle time is more useful for calculating achievable production output.
8. Common Problems and Troubleshooting
| Problem | Possible cause | Recommended action |
|---|---|---|
| Uneven cleaning | Poor part spacing, blocked surfaces, or unsuitable wheel positioning | Adjust the loading arrangement and verify abrasive coverage |
| Rust or mill scale remains | Insufficient exposure time, low abrasive flow, or worn wheel components | Check wheel condition, abrasive supply, and cycle settings |
| Excessive abrasive consumption | Abrasive leakage, poor separation, or unsuitable abrasive grading | Inspect seals, separator settings, and abrasive quality |
| High dust emissions | Damaged seals, clogged filters, or inadequate extraction | Inspect the dust collector, ducting, seals, and filter condition |
| Excessive machine vibration | Worn or unbalanced wheel components, loose fasteners, or bearing problems | Stop the machine and inspect according to the maintenance procedure |
| Inconsistent results between batches | Changes in loading density, abrasive condition, or initial surface condition | Standardize loading and monitor process parameters |
| Slow production output | Long handling time, unsuitable batch size, or inadequate blasting capacity | Review the complete cycle and consider a revised hook or wheel configuration |
Always isolate electrical and mechanical energy before inspection or maintenance, and follow the manufacturer’s lockout and safety procedures. Never open the blasting chamber while the blasting wheels or other hazardous moving components are operating.
9. Maintenance Tips for Stable Blasting Performance
A hook type shot blasting machine operates under abrasive wear. Routine inspection is essential to maintain cleaning quality and reduce unplanned downtime.
Recommended maintenance checks include:
- Blasting wheels: Inspect blades, control cages, impellers, and other wear components at the intervals specified by the manufacturer.
- Hook and hoist: Check load-bearing parts, lifting devices, hook rotation, and safety devices.
- Abrasive system: Monitor abrasive quantity, grading, contamination, and separation performance.
- Dust collector: Inspect filters, differential pressure where applicable, dust discharge, and duct connections.
- Chamber protection: Check liners and other wear-resistant components for excessive wear or damage.
- Electrical controls: Test door interlocks, emergency stops, and other safety functions according to the maintenance schedule.
Maintenance intervals should be based on operating hours, abrasive type, production conditions, and the equipment manufacturer’s instructions.
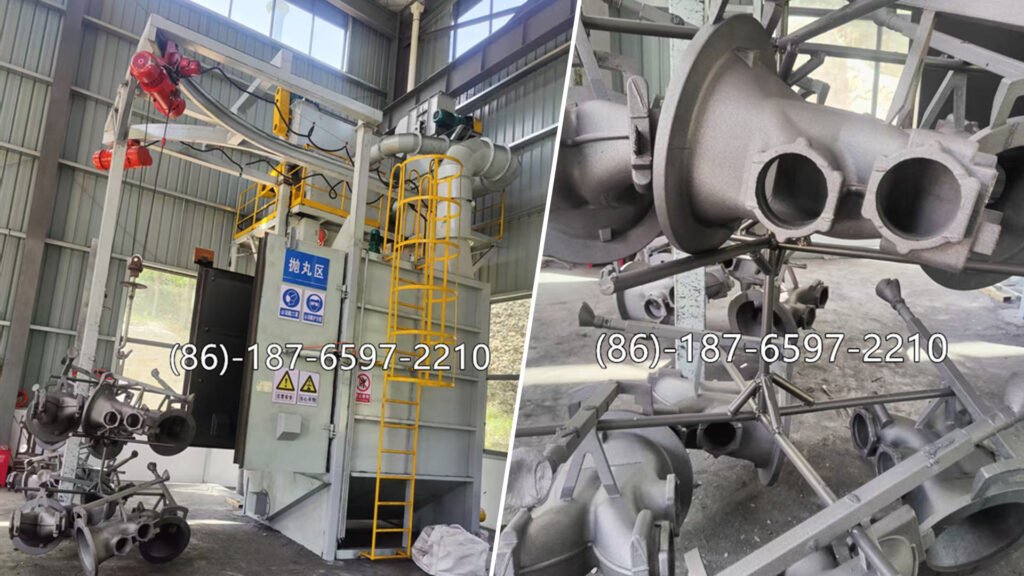
10. Why Choose a Customized Hook Type Shot Blasting Machine?
A standard machine may be suitable for common components, but some production requirements need a customized configuration.
Customization may include:
- Larger chamber dimensions for oversized workpieces
- Higher hook load capacity
- Single-hook or double-hook arrangements
- Multiple blasting wheels for improved coverage
- Customized hooks, fixtures, or baskets
- Dust collector capacity matched to the installation
- PLC controls and production-line integration
- Customized voltage, electrical components, and safety features
For export projects, confirm the installation layout, electrical supply, applicable safety requirements, consumable availability, and maintenance access before production begins.
The objective is not to select the largest machine. It is to select a configuration that achieves the specified surface condition at a practical operating cost.
11. Frequently Asked Questions
Q1: What materials can a hook type shot blasting machine clean?
It is commonly used for cast iron, carbon steel, steel castings, forgings, welded steel structures, and many other metal components. The suitable abrasive and process settings depend on the material and required surface condition.
Q2: Can a hook type shot blasting machine achieve Sa 2½?
It can be configured for applications requiring Sa 2½, provided the machine, abrasive, loading arrangement, and operating parameters are suitable. The result must be verified against the applicable inspection criteria; it should not be assumed from the machine type alone.
Q3: What is the maximum loading capacity?
It depends on the model and configuration. Different Q37 machines can range from hundreds of kilograms to several tonnes per hook. Confirm the rated load, workpiece envelope, and fixture weight with the supplier.
Q4: Is a hook type shot blasting machine suitable for aluminum parts?
It may be suitable for certain aluminum components, but abrasive selection, impact intensity, and surface requirements must be evaluated carefully. Steel shot is not automatically appropriate for every non-ferrous application.
Q5: How long does one blasting cycle take?
There is no universal cycle time. It depends on rust or scale thickness, component geometry, batch loading, abrasive flow, required cleanliness, and handling time. A representative workpiece test is the most reliable way to estimate cycle time.
Q6: What information is required for a quotation?
Provide the workpiece material, maximum dimensions, maximum individual weight, total batch weight, required surface cleanliness, expected production output, power supply, and installation constraints. Photos or drawings help the manufacturer recommend a suitable configuration.
Q7: How can I reduce the operating cost?
Maintain the blasting wheels, monitor abrasive condition, prevent abrasive leakage, maintain the separator and dust collector, and optimize loading and cycle time. The best cost comparison considers labor, energy, abrasive consumption, wear parts, maintenance, and production output together.
12. Get a Hook Type Shot Blasting Machine Solution for Your Production Line
If your factory needs to remove rust, mill scale, casting sand, or other contaminants from metal parts, selecting the correct hook type shot blasting machine can help standardize surface preparation and improve production efficiency.
Instead of choosing a machine based only on a catalogue model, start with the actual workpiece dimensions, loading weight, surface cleanliness requirement, and required daily output.
Contact Bestech to discuss your application and request a suitable machine configuration.
To help us recommend the correct model, please provide:
- Workpiece material: Cast iron, carbon steel, alloy steel, aluminum, or other material.
- Maximum dimensions: Diameter × height or length × width × height.
- Maximum loading weight: Individual part weight and total batch weight.
- Surface preparation target: Rust removal, mill-scale removal, casting cleaning, or a specified grade such as Sa 2½.
- Production requirement: Batches per shift, parts per hour, or tonnes per day.
- Installation details: Available workshop space, power supply, and dust collection requirements.
Send your workpiece photos or drawings for a more accurate recommendation. The machine configuration, expected cycle time, abrasive system, and dust collector can then be evaluated against your production requirements.
Request a Technical Proposal: Get a model recommendation, preliminary technical parameters, and a configuration matched to your workpieces.